The sustainable aviation fuel production process is not one fixed flowsheet. Producers can convert lipids, solid biomass, alcohols, or renewable hydrogen and captured CO₂ into jet-range hydrocarbons through different technology families. Each route has its own feed preparation, reaction sequence, upgrading requirement, utility demand, certification pathway, and scale-up risk.
How is sustainable aviation fuel produced in practice? Every project must complete four basic jobs: prepare a traceable feedstock, convert its carbon into hydrocarbons, adjust molecular structure and boiling range to meet turbine-fuel properties, and qualify the resulting blending component under the applicable fuel specification. HEFA, gasification with Fischer–Tropsch synthesis, alcohol-to-jet, and power-to-liquid reach that endpoint through very different equipment and economics.
The Production Process at a Glance
A complete process begins before the reactor and ends after laboratory testing. The following sequence is broad enough to apply across the major sustainable aviation fuel production methods, although the equipment and contaminants differ by route.
Feedstock qualification — verify origin, composition, variability, traceability, and the lifecycle methodology required by the target market.
Feed preparation — remove water, solids, salts, metals, sulfur, nitrogen compounds, tars, or other route-specific catalyst poisons.
Primary conversion — deoxygenate oils, gasify solids, dehydrate alcohols, or combine renewable hydrogen with captured carbon.
Carbon-chain construction and upgrading — build, crack, hydrogenate, and isomerize molecules into the jet-fuel boiling range.
Separation and fractionation — separate gases and water, recover hydrogen where applicable, and divide naphtha, jet, and diesel fractions.
Testing, blending, and release — confirm route-specific properties, blend within the permitted limit, and verify the finished fuel against the required aviation specification.
Feedstock eligibility and technical approval are separate tests. ASTM approval confirms that a defined conversion route can produce a safe synthetic blending component. Sustainability frameworks separately examine feedstock origin, traceability, lifecycle greenhouse-gas emissions, land-use effects, and other environmental criteria.
Sustainable Aviation Fuel Production Methods Compared
ICAO currently lists 11 approved conversion processes, including several variants of FT, HEFA, ATJ, SIP, catalytic hydrothermolysis, and refinery co-processing. The industry often groups them into four major technology families because those families reveal the largest differences in plant design and resource requirements (ICAO, 2026).
Major route families and their process logic
| Route family | Typical feedstock | Main process chain | Commercial position | Primary constraint |
|---|---|---|---|---|
| HEFA | Used cooking oil, animal fats, eligible plant and waste oils | Pretreatment → hydrodeoxygenation → hydrocracking/isomerization → fractionation | Most commercially mature | Eligible lipid supply, hydrogen, and feed variability |
| Gasification + FT | Agricultural and forestry residues, selected municipal waste, other carbonaceous feedstocks | Preparation → gasification → syngas cleanup → FT synthesis → product upgrading | Certified; limited commercial deployment for waste and biomass | Capital cost, feed logistics, gas cleanup, and availability |
| ATJ | Ethanol, isobutanol, and other alcohols covered by the applicable route | Purification → dehydration → oligomerization → hydrogenation → fractionation | Early commercial scale-up | Alcohol cost and carbon intensity, hydrogen, and conversion yield |
| PtL / e-SAF | Renewable electricity, water, and captured CO₂ | Electrolysis → CO₂ conversion → syngas or methanol → synthesis and upgrading | Demonstration and early project development | Clean-power cost, utilization, efficiency, CO₂ source, and certification route |
HEFA: Converting Fats and Oils
HEFA feedstocks first undergo filtration, degumming, drying, and contaminant removal appropriate to the incoming oil. The cleaned lipids react with hydrogen to remove oxygen, mainly as water and, depending on catalyst and conditions, as carbon monoxide or carbon dioxide. This creates long paraffinic molecules. Hydrocracking and hydroisomerization then adjust chain length and branching so the product can meet jet-range boiling and low-temperature requirements. Fractionation separates jet fuel from renewable diesel, naphtha, and lighter products.
The central trade-off is jet yield versus cracking severity. More severe upgrading can improve the jet fraction’s cold-flow properties but can also create additional light products. Feed quality, hydrogen consumption, product slate, and catalyst life therefore have to be optimized together. This article keeps HEFA at comparison depth; the detailed lipid pretreatment, hydrogen loop, and catalyst sequence belongs in JALON’s separate HEFA process guide.
Gasification and Fischer–Tropsch: Rebuilding Carbon from Syngas
Gasification routes begin with solids rather than liquids. Biomass or waste must be sorted, sized, dried, and sometimes densified before entering the gasifier. Heat, oxygen, and steam convert the material into synthesis gas containing hydrogen, carbon monoxide, carbon dioxide, methane, particulates, tars, sulfur compounds, nitrogen species, and trace contaminants. The cleanup train is essential because FT catalysts require tightly controlled syngas quality.
After cleanup, the hydrogen-to-carbon-monoxide ratio is adjusted for synthesis. Fischer–Tropsch catalysts build long hydrocarbon chains from the syngas; hydrocracking and isomerization then convert waxes and heavier products into jet-range molecules. The route can use abundant residues that are unsuitable for HEFA, but a project must manage heterogeneous feed, solids logistics, oxygen demand, gasifier reliability, syngas purification, and a capital-intensive upgrading section. “Any biomass” is therefore not an adequate feed specification.
Alcohol-to-Jet: Building Longer Chains from Alcohols
ATJ starts with a purified alcohol whose origin may be biological, waste-derived, or synthetic. Dehydration converts the alcohol into its corresponding alkene: ethanol becomes ethylene, while isobutanol becomes isobutene. Oligomerization joins those small molecules into longer chains, hydrogenation saturates the products, and fractionation isolates the desired jet range. Depending on the route and product distribution, further isomerization or finishing may be required.
This pathway can use existing alcohol-production and logistics infrastructure, but the carbon intensity of the alcohol matters as much as the upgrading plant. Fermentation energy, agricultural inputs, land-use assumptions, electricity, hydrogen, carbon capture, and transport can all change the lifecycle result. Project evaluation should therefore connect the alcohol plant and the ATJ plant in one mass, energy, and emissions model rather than treating purchased ethanol as a uniform commodity.
Power-to-Liquid: Combining Renewable Hydrogen and Captured Carbon
PtL uses renewable electricity to produce hydrogen by water electrolysis. Captured CO₂ is cleaned and compressed, then combined with hydrogen through a conversion step such as reverse water-gas shift to make syngas or through methanol synthesis. The intermediate can then be converted through FT, methanol-derived chemistry, or another qualified pathway and upgraded into jet-range fuel.
PtL is not itself a single ASTM annex and should not be assigned one universal blending limit. Certification follows the downstream conversion route used to make the synthetic blending component. The climate performance is also conditional: electricity carbon intensity, electrolyzer utilization, hydrogen compression, CO₂ source, conversion efficiency, and heat integration all matter. Cheap electricity alone does not guarantee a competitive or low-carbon e-SAF plant.
Common Process Blocks Across Different Routes
Feed Preparation Protects the Conversion Section
Each route arrives with a different impurity profile. Lipids can contain water, phosphorus, salts, metals, free fatty acids, and oxidation products. Biomass-derived syngas can contain particulates, tars, sulfur, ammonia, chlorides, alkalis, and excess carbon dioxide. Alcohol feeds may contain water and fermentation by-products. Captured CO₂ and electrolytic hydrogen require purity and moisture control appropriate to the synthesis process.
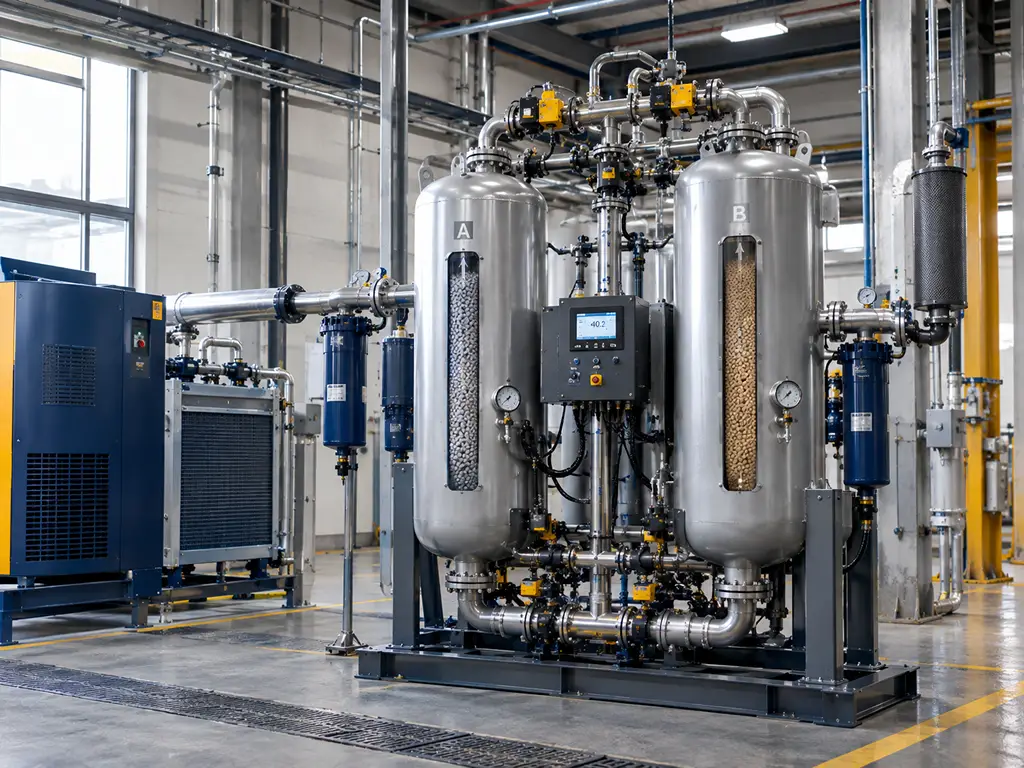
These streams should not be assigned one universal adsorbent or guard-bed configuration. The correct design follows measured composition, pressure, temperature, flow, contaminant loading, required outlet specification, and regeneration strategy. Treating an adsorbent grade as standard merely because it appeared in another SAF flowsheet can transfer contamination risk into a much more expensive catalyst section.
Upgrading Creates Jet-Fuel Properties
Primary conversion rarely produces a finished jet blend component directly. HEFA and FT products often contain straight paraffins or heavy waxes that require controlled cracking and isomerization. ATJ must build longer chains from small alkenes and then hydrogenate them. PtL inherits the upgrading requirements of its selected downstream route.
Cold-flow performance is one reason this stage matters. Jet A and Jet A-1 have different maximum freeze-point requirements, commonly −40°C and −47°C respectively. Increasing molecular branching generally improves low-temperature behavior, but excessive hydrocracking reduces jet yield by shifting material into naphtha and light gases. Catalyst selectivity, temperature, hydrogen pressure, space velocity, and feed purity must therefore be evaluated as a system rather than optimized one at a time.
Fractionation Determines the Saleable Product Slate
A SAF plant normally produces more than one hydrocarbon fraction. Distillation and gas separation divide light gases, naphtha, jet-range material, diesel-range material, unconverted intermediates, water, and recycle streams. The economic model must use realistic yields for all co-products instead of assuming every tonne of feed becomes aviation fuel. A renewable-fuels plant may also change operating severity to favor diesel or jet production as relative prices and policy values move.
How to Choose a Sustainable Aviation Fuel Technology
The route should be selected from the site’s strongest resource advantage and its weakest constraint. Feedstock price alone is insufficient because transport radius, variability, storage, preprocessing, utilities, financing, certification, and product flexibility can reverse an apparent cost advantage.
| Selection factor | Questions to answer | Why it changes the route decision |
|---|---|---|
| Feedstock and logistics | What annual volume is traceable? How variable is composition? What transport and storage are required? | Determines pretreatment load, plant scale, utilization, and lifecycle result |
| Utilities | Are hydrogen, low-carbon electricity, oxygen, steam, water, and CO₂ available at the required quality? | Can dominate both operating cost and emissions |
| Existing assets | Can refinery, alcohol, gasification, hydrogen, storage, or blending infrastructure be reused? | Changes capital cost, schedule, integration risk, and product flexibility |
| Technology maturity | Is the proposed scale supported by operating references, warranties, and licensor data? | Controls commissioning risk, financing terms, and ramp-up assumptions |
| Lifecycle carbon | Which methodology and certificate scheme apply? What assumptions cover land use, power, hydrogen, and co-products? | Determines whether the product earns the intended regulatory or voluntary value |
| Product and certification | Which ASTM annex applies? What blend limit, aromatic content, product slate, and target market are required? | Sets the testing program and revenue model |
A lipid-rich region with refinery hydrogen may favor HEFA. A site controlling large, consistent residue streams may justify gasification-FT. Established low-carbon alcohol supply can support ATJ. PtL becomes more credible where renewable power is abundant, electrolyzers can operate at high utilization, and a suitable CO₂ source is secured. These are starting conditions, not automatic answers; bankable selection still requires site-specific mass and energy balances.
Certification, Blending, and Sustainability Qualification
ASTM D7566 contains annexes for approved synthetic aviation-fuel blending components. Each annex defines eligible process conditions, composition requirements, and maximum blend ratio. Widely deployed HEFA-SPK, FT-SPK, and ATJ-SPK routes allow blends up to 50%, while SIP and HC-HEFA-SPK are limited to 10%. ICAO also lists D1655 co-processing routes with different limits, including 5% for certain fats, oils, greases, and FT hydrocarbons, and 10% for a defined HEFA co-processing route (ICAO, 2026).
After the approved synthetic component is blended and the finished batch meets the applicable specification, it can be reidentified as conventional specification-compliant jet fuel. Demonstration flights using 100% SAF do not remove today’s route-specific commercial blend limits. Broader unblended use requires additional qualification of fuel properties, material compatibility, combustor operability, emissions, and handling performance.
Technical compliance alone does not establish a sustainability claim. CORSIA and regional systems impose separate rules for lifecycle emissions, eligible feedstocks, traceability, certification, and verification. A project should identify its target market and accounting system before freezing feed contracts or process design.
Where Production Projects Commonly Go Wrong
Announced capacity is treated as production.
Nameplate capacity does not account for delayed commissioning, low utilization, feedstock shortages, or a refinery choosing renewable diesel instead of SAF.
The feedstock specification is too broad.
“Waste oil,” “biomass,” or “captured CO₂” is not enough. Variability and contaminants determine pretreatment, catalyst exposure, yield, and downtime.
Laboratory yield becomes the financial model.
Commercial balances must include product separation, recycle, catalyst aging, startup losses, downtime, co-products, and off-spec material.
Certification is left until the end.
The exact feedstock, process route, annex, blend limit, testing program, and target certificate scheme must be identified during project definition.
Adsorbents and catalysts are selected from generic datasheets.
Static capacity or surface area does not establish working performance under the project’s actual pressure, temperature, contaminants, and regeneration cycle.
Specifying Purification and Catalyst Materials
Material selection begins with a stream specification. For a drying or purification duty, the RFQ should state composition, phase, pressure, temperature, normal and maximum contaminant loading, required outlet level, flow range, cycle time, regeneration method, particle-size constraint, allowable pressure drop, and mechanical-strength requirement. For zeolite-containing catalyst materials, framework type, silica-to-alumina ratio, crystal size, acidity, binder system, metals, and activation procedure may all affect performance.
JALON can support the initial screening of zeolite materials and molecular-sieve products for SAF-related applications. Share the actual stream conditions, target product properties, and licensor requirements so the technical team can identify candidate grades, provide available characterization and batch documentation, and define an appropriate sample-validation plan. Final material approval should remain tied to application-specific testing and the process licensor or EPC design basis.
Review the Material Requirements for Your SAF Route
Send the feed composition, process conditions, contaminants, target outlet specification, and regeneration requirements for an initial technical review.
Discuss Your Process ConditionsReferences
- International Civil Aviation Organization. SAF Conversion Processes. Accessed 2026.
- U.S. Department of Energy. Pathways to Commercial Liftoff: Sustainable Aviation Fuel. 2024.
- U.S. Department of Energy. Sustainable Aviation Fuel: Review of Technical Pathways. 2020.
- U.S. Department of Energy, Alternative Fuels Data Center. Sustainable Aviation Fuel. Accessed 2026.
- International Air Transport Association. Sustainable Aviation Fuel. 2026.
- National Renewable Energy Laboratory. Sustainable Aviation Fuel State-of-Industry Report. 2024.
- ASTM International. ASTM D7566: Standard Specification for Aviation Turbine Fuel Containing Synthesized Hydrocarbons.

 EN
 DE
 ES
 JA
 RU
 PT
 FR
 AR
 KO
 TH
 ID